
Restoring Cycle Time: How to Clean Clogged Injection Mold Cooling Channels
The Hidden Bottleneck in High-Speed Thin-Wall Molding
In high-speed injection molding, cooling accounts for up to 70% of the total cycle time. When hard water calcium scale and iron rust choke your internal cooling circuits, heat transfer drops drastically. This extends a stable 5-second cycle time to 8 seconds or more, silently draining your factory’s daily profits.
Below is a real-world maintenance case study from Daya Machinery showing how we diagnosed, flushed, and restored a 4-cavity food container mold to peak efficiency.
Phase 1: Borescope Diagnosis (The Problem)
Before flushing, our technical team used an industrial borescope to inspect the internal water channels.
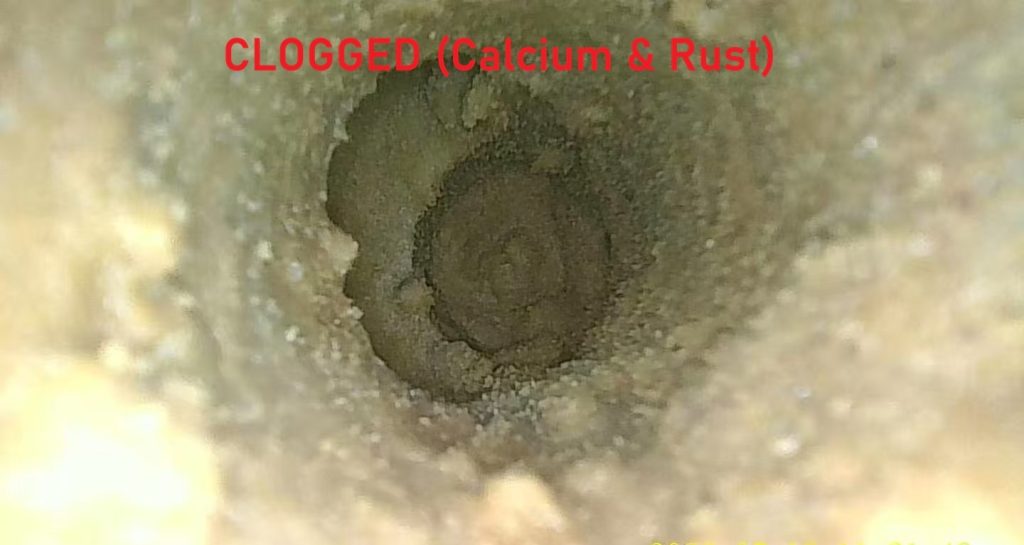
Caption: Internal view showing heavy calcification and corrosion blocking water flow.
As shown above, years of untreated hard water caused severe calcium carbonate scale and rust scaling. The pipe diameter was restricted by over 50%, causing uneven cooling and part warping.
Phase 2: High-Velocity Chemical Descaling (The Action)
To dissolve the blockages without damaging the mold steel, we connected our specialized high-velocity chemical descaling pump system directly to the mold manifolds.
[ MOLD MANIFOLDS ] <=======(Orange Reinforced Hoses)======= [ DESCALING PUMP SYSTEM ]
       ||                                                               ||
       V                                                                V
  Restricted Flow                                                Active Acid Agent
(Diagram: Closed-loop chemical flushing setup used on the factory floor)

Once the specialized organic descaling acid agent was introduced, it triggered an immediate reaction with the calcium scale.
Caption: Watch the video to see the chemical foaming action actively dissolving and suspending the internal industrial sludge.
Phase 3: 100% Clear Channels & Full-Speed Production (The Result)
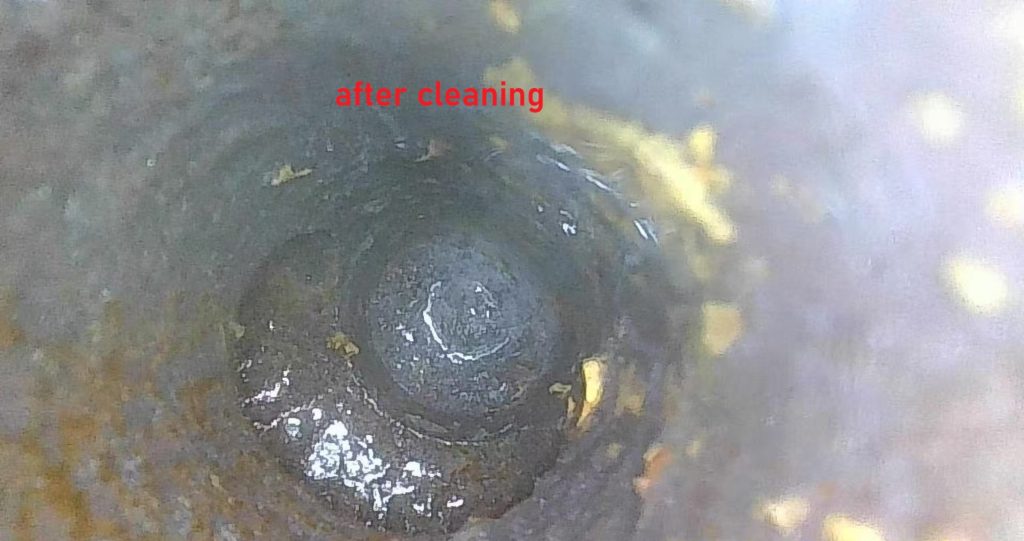
After 90 minutes of continuous loop-flushing and a final neutral clean-water rinse, the results were definitive.
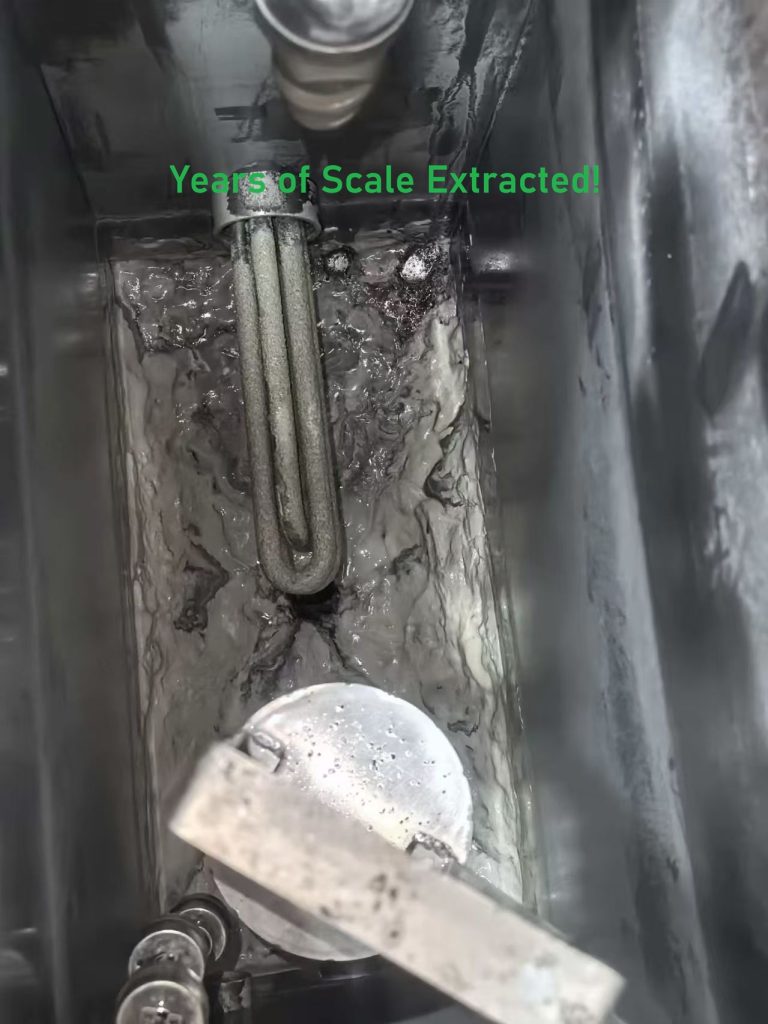
Sludge Extracted: A thick layer of heavy industrial gunk was pulled completely out of the circuit.
Internal Surface: Borescope inspection confirmed a clean, bare-metal pipe surface with zero restrictions.
Production ROI Recovery Matrix
| Performance Metric | Before Descaling | After Daya Descaling | Net Result |
| Internal Scale Buildup | Severe restriction (>50% choked) | 100% Cleared (Bare metal) | Restored Flow |
| Cooling Efficiency | Reduced by ~40% (Uneven) | 100% Thermal Transfer | Stable Parts |
| Mold Production Cycle | 8.2 Seconds (Delayed) | 5.1 Seconds (Optimized) | +38% Speed Boost |
Once re-mounted to our high-speed injection molding machine, the 4-cavity thin-wall packaging mold immediately resumed stable, high-volume production with zero dimension defects.
Need to Optimize Your Packaging Production Line?
Daya Machinery supplies top-tier high-speed injection machines, precision packaging molds, and full auxiliary setup support globally.
📬 Contact Kyle Ge for Technical Support & Turnkey Quotes:
Email: sales@dayamachinery.com
WhatsApp / WeChat: +86-13884490945
Official Website: www.dayamachinery.com